
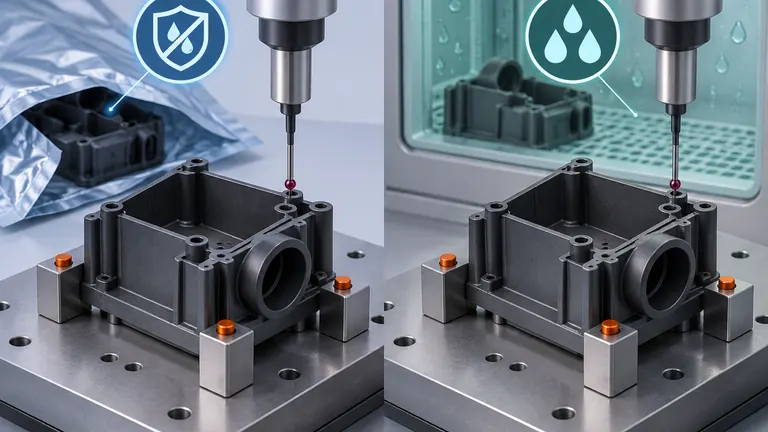
Conceptual illustration; not to scale.
A nylon part can pass a dimensional report immediately after molding and fail a later report after it absorbs moisture. The reverse can also happen when a buyer compares a conditioned sample with a dry-as-molded production check. If the drawing does not state which state governs acceptance, both parties may be measuring correctly and still disagree about whether the part is conforming.
Neither dry-as-molded nor conditioned acceptance is universally correct. Accept the state that represents the part’s controlled function and customer requirement, and document the material grade, moisture or conditioning protocol, environment, timing, packaging and measurement method. If the part must function across states, define the applicable limits or verification sequence for each state. Do not invent a universal conditioning time, moisture percentage or dimensional-change allowance for all nylon grades.
This article focuses on dimensional acceptance. It does not replace a material-selection review or a durability, sealing or electrical validation plan.
Why nylon state must be treated as a product variable
Why this matters: “Nylon” is a family description, not a complete dimensional specification. Different polyamide families, reinforcement levels, additives, colors, molding histories and wall geometries can respond differently to moisture and temperature. A dry-as-molded report is a snapshot of a freshly processed state; a conditioned report describes a different state of the polymer and often a different mechanical response.
The material supplier’s data should be the starting point. Obtain the exact manufacturer and grade, reinforcement type and level, color or additive package, approved alternate status, processing guidance and relevant moisture-conditioning information. BASF’s Ultramid documentation explains that standard injection molding grades can reach more stable dimensions and optimum impact behavior after moisture absorption, and that conditioning time depends strongly on wall thickness and the selected conditions. That guidance is grade-family information, not permission to copy a target onto another PA grade.
Geometry also changes the response. A thin wall may equilibrate differently from a thick boss. A glass-filled part can have direction-dependent shrinkage and moisture response. A long flow path can create orientation that makes one axis respond differently from another. The feature that matters for assembly may therefore move more or less than a free outside dimension. Use a dimensional study on the actual part, not only a resin datasheet, when the acceptance margin is small.
The business question is which state the customer receives and which state the component sees when it performs its function. If the supply chain packages a part soon after molding but the vehicle environment allows moisture uptake, a dry-only release may not protect the installed function. If a component is installed rapidly and the drawing explicitly defines as-molded geometry, conditioning may be a development check rather than a lot-release criterion. Both decisions can be reasonable when they are intentional and documented.
The state can also influence the test method itself. A dry part may be stiffer and easier to fixture, while a moisture-exposed part may deflect more under a probe or clamp. If the acceptance condition changes the part’s support behavior, document the fixture state together with the material state. Compare the same feature in the same direction and use the same datum setup. Otherwise a report may attribute a fixture or operator difference to polymer moisture. This is why a grade-specific study and a controlled handoff are more defensible than a copied rule for all nylon parts.
Select the acceptance state from the function and supply chain
Why this matters: Start with the service and assembly sequence. Identify whether the critical dimension controls immediate assembly, long-term clearance, retention, sensor position or a later subassembly. Then identify when that function is evaluated: at the molding site, at a customer plant, after storage, during vehicle assembly or in service. The acceptance state should represent that decision, subject to customer requirements.
Consider three possible models. In a dry-as-molded model, the supplier measures after a defined post-mold stabilization and before significant moisture exposure. In a conditioned model, the supplier follows a specified material- and part-relevant conditioning process before measuring. In a two-state model, the team defines a dry state for handling or initial assembly and a conditioned or environmental state for the functional dimension. The two-state model may need more samples and a wider evidence plan, but it can be the honest choice when the part operates across environments.
Do not confuse “dry” with “drying the pellets.” Resin drying is a processing requirement that protects melt quality. Dry-as-molded describes the moisture state of the molded part at measurement. A part can be molded from correctly dried pellets and still absorb moisture after molding. Likewise, conditioning the part is not the same as heating it to remove moisture. Use distinct words in the drawing and report.
For each critical feature, ask whether the tolerance applies to a size, location, profile or function. If a connector must fit after conditioning, measure the connector interface in the conditioned state or define both states. If a bracket hole is installed with a clamp that absorbs a small shift, the assembly fixture may be the correct verification. If the feature is a cosmetic edge, define visual and free-state conditions rather than assuming the same dimensional state as an internal fit.
Customer-specific requirements control when they exist. AIAG PPAP or an OEM submission requirement may request representative production parts and specific dimensional evidence, but the applicable sample state and test conditions still need to be agreed in the project documents. The supplier should not select the state solely because it is easier to measure.
Make the decision visible in the control plan. The supplier, customer plant and assembly team should know which state is used for first-off release, which state is used for periodic verification and which state is used for a functional investigation. If the customer has not defined the state, state the proposal as an assumption and request disposition before production release. The point is not to create more checks automatically; it is to ensure that every required check describes the condition in which the part must work.
Record material, environment and timing without false precision
Why this matters: The most common mistake is a report that says “conditioned” without saying how. The word can describe different temperature, humidity, exposure, packaging and stabilization sequences. A second mistake is reporting a moisture percentage as if it were a universal acceptance target when the grade supplier provides only grade-specific information.
Capture the exact resin, part state, temperature, humidity, time, packaging, fixture, measurement method and governing acceptance basis so another inspector can reproduce the result.
Use an acceptance-condition record for every development and production check:
| Record item | What to capture | Why it matters |
|---|---|---|
| Material identity | Manufacturer, exact grade, color, reinforcement, lot and approved revision | Similar polymer names do not guarantee similar moisture or shrinkage behavior |
| Molding state | Machine, mold, cavity, process revision and time from ejection | Process history and post-mold time affect the measured baseline |
| Part state | Dry-as-molded, conditioned, stored, assembled or two-state sequence | The label must describe the actual acceptance condition |
| Temperature | Chamber, part and measurement-room temperature | Thermal expansion and part flexibility can change the result |
| Relative humidity | Exposure and measurement-room humidity where applicable | Moisture uptake is environment-dependent |
| Time | Ejection-to-measurement and conditioning or stabilization interval | An interval without a defined start and end cannot be reproduced |
| Packaging | Bag, desiccant, open tray, sealed container or shipping simulation | Packaging controls exposure between molding and inspection |
| Fixture state | Free, gravity-supported, clamped or functionally assembled | Restraint can hide or create deformation |
| Measurement method | CMM, vision, gage, scan, contact force and datum setup | Different methods may measure different physical conditions |
| Acceptance basis | Drawing revision, TDS, customer requirement or approved study | Evidence must be tied to the requirement that governs the decision |
Use the table as a release record, not as a substitute for the drawing. The drawing should state the required state or reference the controlled procedure. The report should state what actually happened. If a deviation occurs, record it and obtain the required disposition; do not silently rename the state after seeing the result.
The receiving inspector should be able to reconstruct the condition from the record without asking the molder to remember it. State whether the chamber or room log is the controlling evidence, how the sample container was identified, and what happens when the measured state is not achieved. If the project accepts a study result for one grade but not an alternate grade, list that boundary. When the record is attached to a PPAP or customer submission, the evidence index should link the condition log to the dimensional report and to the material identity. This makes a later dispute about a changed dimension testable rather than argumentative. Also record sample orientation, cavity identity, measurement timestamp, package opening time and any interruption in conditioning. If an operator transfers the samples between rooms, note the transfer and the temperature equalization period. These details let quality distinguish a true material-state effect from a handling event. Keep the record with the sample labels and raw measurement file, not only in a summary spreadsheet.
Control storage and measurement so results remain comparable
Why this matters: Nylon parts continue to exchange moisture with their environment. That makes handling between molding, packaging, transport and measurement part of the measurement system. A part measured after an open-table delay is not necessarily comparable with a sealed part measured immediately after unpacking.
Define the handoff. At ejection, place samples in a labeled container with cavity, time and material lot. For dry-as-molded acceptance, limit additional exposure and state the stabilization time. For conditioned acceptance, use the supplier’s grade-specific or customer-approved protocol and record start, end, temperature, humidity and achieved state. Avoid water immersion or elevated temperature as a generic shortcut when the material supplier warns that the method can create stains, warpage or surface effects for particular grades or geometries.
Measurement room conditions matter as much as chamber conditions. Allow the part and fixture to reach the agreed measurement temperature. Keep the same support points and contact force. A thin housing can deflect under a CMM probe or when pressed onto a nest. If a fixture is needed, define the contact sequence and clamp condition, and verify that the fixture does not force an out-of-shape part into a passing position.
Use a reference sample and a repeated method during the study. Compare multiple cavities and relevant flow directions rather than using a single convenient sample. The study should separate short-term repeatability, cavity-to-cavity variation, process variation and state-related movement where practical. If a result is near a specification limit, measurement uncertainty and the agreed decision rule must be considered. ISO 14253-1 provides a framework for conformity decisions that accounts for uncertainty close to limits; it does not tell a project what acceptance state to choose.
For production, place the state and timing in the control plan or inspection instruction. Include a reaction when the state cannot be confirmed, when packaging is damaged or when the measurement room is outside the agreed range. A report with more decimal places is not more reliable if the part state is unknown.
Use labels that travel with the samples: part number, drawing revision, resin lot, cavity, molding timestamp, state, condition start and end, package and measurement timestamp. Retain raw data when a result is close to a limit. If the result changes after the part is moved between rooms, investigate the state and temperature before changing the mold. A stable inspection instruction should also say what happens when a package is opened accidentally or a chamber record is incomplete.
Write an acceptance clause that can survive a handoff
Why this matters: The drawing or controlled quality document should answer five questions: Which grade is being accepted? What part state applies? What environment and stabilization apply? How is the part located and measured? Which document or customer instruction governs exceptions?
An effective clause might say that the characteristic is accepted on parts of the specified grade and revision, measured in the defined free or constrained state, after the identified stabilization or conditioning procedure, within the stated temperature and humidity range, using the named datum setup and method. It should point to the source procedure and revision rather than embedding an unverified universal number. If both dry and conditioned states matter, list the features and limits for each state or define a sequence of tests.
The clause should not say “measure after conditioning” and stop. The supplier needs the approved protocol, sample quantity, cavity representation, storage container, report fields and reaction plan. Quality needs to know whether a failed dry check but passing conditioned check is a product nonconformance, a development finding or a measurement-state mismatch. Purchasing needs to know whether the additional conditioning and inspection work is included in the RFQ.
Illustrative example: an under-hood PA housing includes a connector interface and a screw boss. The project learns that the connector is assembled after transport, while the boss is checked during initial supplier inspection. The team defines dry-as-molded inspection for the launch check and a separate conditioned study for the connector interface because the installed function must be understood after moisture exposure. The condition record identifies the exact grade and the supplier’s approved procedure. No generic moisture target or universal conditioning duration is published in the drawing.
If the measured change is larger than the available tolerance, the answer is not automatically a tighter process. Review grade, fiber orientation, wall design, fixture restraint, assembly function and customer limits. A design or material decision may be needed before a tooling correction. Link the result to automotive injection molding materials and the automotive quality and validation route when the evidence needs to be converted into a launch control.
The clause should also identify who may change the condition. A supplier may recommend a different humidity or stabilization method, but the change should be approved against the material supplier’s information, the customer requirement and the functional risk. Keep the original condition as the baseline in the report. This prevents a later lot from being compared with a result obtained under a different state and described by the same short word.
Conclusion
Choose the acceptance state from the part’s function and supply chain, then document exact material identity, state, environment, timing, packaging, fixture and measurement method. Use grade-specific supplier data and an actual-part study; never copy a universal nylon conditioning time or moisture target. Include the condition record with the drawing and RFQ.
References
- BASF, Ultramid brochure — moisture absorption, conditioning and wall-thickness-dependent timing for Ultramid grades.
- BASF, Product Information for Ultramid B3Z1 — grade-specific product and storage information.
- ISO, ISO 14253-1:2017 — measurement uncertainty in conformity decisions.
- NIST, Measurement Uncertainty — measurement conditions and uncertainty concepts.